


Explore our heavy-duty, certified industrial racking options engineered for global B2B supply chains, cold storage facilities, and automated logistics hubs.
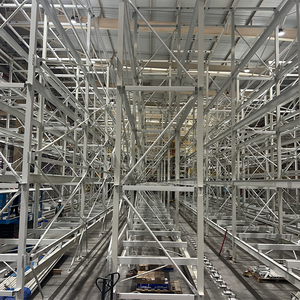
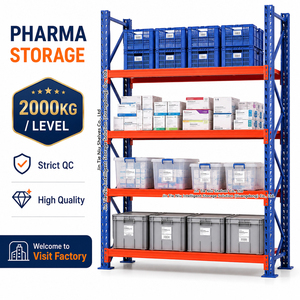
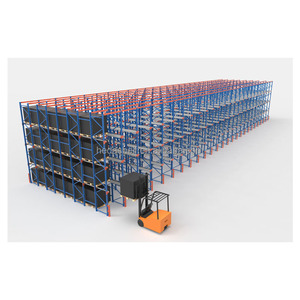
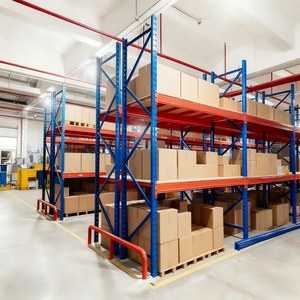
Why Tier-1 logistics centers, pharmaceutical distributors, and automotive manufacturers choose China's leading wholesale OEM racking and conveyor exporters.
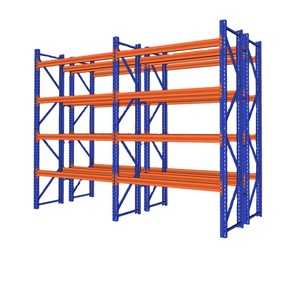
Our industrial pallet conveyor racking systems utilize high-tensile hot-rolled Q235B and Q355B structural steel channels alongside closed-tubular upright designs (such as our flagship SK2000 boltless series). Unlike cheap roll-formed open-profile racking that buckles under localized forklift impacts, closed tubular and structural channel columns possess dramatically elevated torsional rigidity and high moment of inertia.
Every beam-to-frame connector features heavy-duty safety locks and precision CNC-punched indexing to prevent accidental beam dislodgement under violent load movements or automated conveyor line surges.
International procurement managers demand compliance with strict regional safety and engineering specifications. Our structural designs are rigorously calculated in accordance with key global codes:
Every shipment is backed by Finite Element Analysis (FEA) structural validation reports, localized seismic calculation packages, load capacity rating plaques, and full assembly CAD drawings.
Strategic insights for procurement directors preparing their warehouse infrastructure for 2026-2035 supply chain shifts.
Traditional static pallet storage is rapidly giving way to dynamic, live-flow conveyor integration. Modern B2B logistics facilities no longer treat storage racks and conveyor transport lines as separate equipment siloes. Instead, modern high-density warehouses specify Pallet Flow Rack Systems with Integrated Powered Motorized Driven Roller (MDR) Accumulation Conveyors.
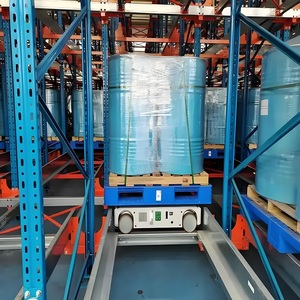
This hybrid approach enables zero-pressure accumulation (ZPA) where 1,000kg+ heavy pallet loads drift safely down gravity lanes controlled by magnetic speed controllers, interfacing seamlessly at the pick face with automated guided vehicles (AGVs) or 4-way radio shuttles.
As market demand fluctuates, fixed infrastructure presents a capital liability. Global buyers are increasingly prioritizing boltless modular racking components that allow quick vertical beam adjustments in 50mm or 75mm increments without structural welding. Combined with integrated mezzanine work platforms, facilities double or triple usable square footage within their existing building footprint.
Procurement specifications now frequently include smart sensing telemetry embedded directly into racking uprights and motor-driven conveyor nodes. Optical sensors monitor pallet placement accuracy, load overhang, roller thermal conditions, and dynamic strain variations, feeding telemetry into warehouse management systems (WMS) for predictive maintenance before mechanical failures occur.
Analyzing key advancements in heavy-load material handling, automated runner shuttles, and protective finishes.
Radio Shuttle automated storage systems allow high-density deep-lane storage (up to 30 pallets deep) while operating in either LIFO (Last-In, First-Out) or FIFO (First-In, First-Out) configurations. The latest 4-way intelligent shuttle runners transfer between rack channels autonomously, eliminating forklift transit within rack aisles and boosting warehouse spatial utilization up to 85%.
For pharmaceutical and sub-zero cold storage operations (-30°C), traditional paint quickly chips and rusts due to condensation cycling. Advanced thermosetting epoxy-polyester electrostatic powder coatings or hot-dip galvanizing (HDG) protect steel against chemical washdowns, severe friction, and thermal shock, extending service life beyond 20 years.
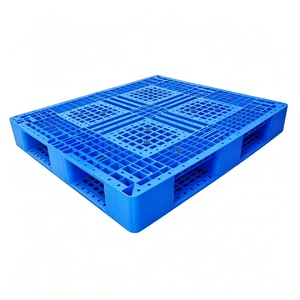
Pallet conveyor systems incorporate custom roller pitch configurations tailored specifically to wood, plastic, or metal pallet bottom runner profiles. Self-energizing magnetic speed controllers automatically regulate pallet descent speeds down gravity lanes, ensuring consistent speed (below 0.3 m/s) regardless of pallet weight variance from 200kg to 1500kg.
A quick engineering reference guide to evaluate capacity, density, and inventory access methodology across common racking structures.
| Storage System Type | Storage Density | Selectivity | Rotation Method | Conveyor Integration | Optimal Use Case |
|---|---|---|---|---|---|
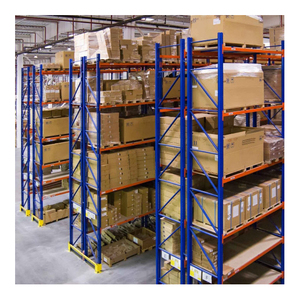
| Selective Pallet Racking | Low - Medium (40%) | 100% Direct Access | FIFO / LIFO | Line-side staging conveyors | High SKU variety, fast-moving consumer goods |
| Pallet Flow / Live Roller Rack | Very High (75%-85%) | Low (Per Lane) | Strict FIFO | Integrated gravity/driven rollers | Perishables, food & beverage, date-sensitive goods |
| Pushback Racking | High (60%-70%) | Medium (Per Lane) | LIFO | Nested cart accumulation | 2 to 6 deep pallet storage, medium SKU count |
| 4-Way Radio Shuttle Rack | Maximum (85%+) | Automated Channel Access | FIFO or LIFO | Fully integrated AS/RS & AGV loops | Cold storage, bulk manufacturing, high throughput |
| Drive-In / Drive-Through | High (65%-75%) | Low | LIFO (Drive-In) / FIFO | Manual forklift entry | Homogeneous bulk items, seasonal inventory |
Addressing the technical, logistics, and quality assurance queries raised by global importers and engineering contractors.
To provide an accurate structural CAD proposal and load calculation sheet, our engineering team requires: (1) Exact pallet dimensions including overhang and bottom runner orientation; (2) Minimum and maximum load weights per pallet; (3) Building clear ceiling height and column spacing grid; (4) Floor slab thickness, concrete grade, and rebar layout; (5) Environmental operating temperatures (ambient, chilled, or sub-zero freezer); and (6) Required throughput speed (pallets moved per hour).
Boltless tubular uprights (such as our SK2000 specification) feature closed, continuous-weld square or rectangular steel tubing. This provides multi-directional torsional rigidity and eliminates open edges that twist when hit by forklift forks. Structural channel racking (SK3000 series), made from hot-rolled C-channels, offers supreme mass and structural strength, ideal for heavy-duty drive-in, pushback, and extreme capacity applications over 2,000kg per level.
Export packing integrity is vital to prevent transit damage. Upright frames, horizontal beams, and conveyor rails are nested, steel-strapped into heavy-duty bundled packs, protected by corrugated corner guards, and wrapped in plastic shrink film. All small structural brackets, bolts, dynamic speed controllers, and hardware are crated in labeled wooden boxes matching the assembly bill of materials (BOM) for easy on-site sorting.
Yes. Our engineering department routinely performs seismic structural calculations based on local building codes (such as US IBC/RMI guidelines or European Eurocode 8). Seismic resilience is achieved using oversized floor baseplates, heavy-duty mechanical wedge anchors, reinforced frame bracing patterns, and high-ductility steel alloys engineered to absorb seismic ground acceleration without structural collapse.
Live gravity flow systems require minimal maintenance: periodic visual inspection of speed control brakes, checking roller bearings for debris, and verifying pallet entry guides are un-damaged. Motorized Driven Roller (MDR) and chain conveyor systems require scheduled lubrication of drive chains, checking belt tensions, and keeping optical sensor lenses clean from dust build-up.
Connect directly with our senior structural engineers and global export team for detailed layout CAD designs, FEA calculations, and factory-direct wholesale pricing.