


Precision-crafted, CE-marked heavy-duty racking engineered specifically for pharmaceutical distribution centers, cold storage rooms, and cleanroom staging areas.
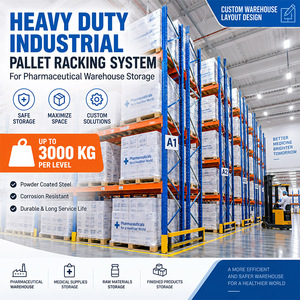
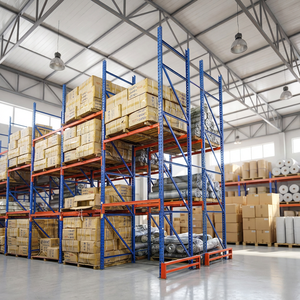
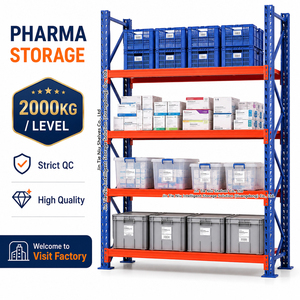
Pharmaceutical logistics demand zero tolerance for structural deflection, contamination risks, or operational downtime. Our proprietary steel rack engineering addresses every strict regulatory standard.
Every racking component undergoes rigorous finite element structural analysis (FEA) compliant with European Standard EN 15512, RMI (ANSI MH16.1), and AS 4084. Certificate of Conformity is issued with structural load plates for full legal and audit compliance.
We utilize non-gassing, anti-microbial epoxy powder coatings and smooth, continuous robot-welded joints. These eliminate micro-crevices where particulate matter, bacteria, or moisture might accumulate, supporting strict ISO 7 and ISO 8 cleanroom environments.
Our flagship closed-section structural tubular uprights offer 44 times more torsional strength than standard open roll-formed steel racks. This engineered impact resistance mitigates forklift collision risks in narrow, high-density pharmaceutical warehouse aisles.
In the highly regulated global life sciences sector—spanning active pharmaceutical ingredients (APIs), finished dosage forms, biologics, vaccines, and medical devices—warehouse storage infrastructure plays an integral role in maintaining product integrity. Storage systems must comply with stringent Good Manufacturing Practice (GMP) and Good Distribution Practice (GDP) directives, including EU GDP 2013/C 343/01 and US FDA 21 CFR Part 211.
As a premier CE-certified pharmaceutical pallet racking manufacturer, our engineering framework merges high-yield structural steel integrity with micro-cleanliness, cold chain performance, and full traceability. Selecting the right racking infrastructure directly impacts facility safety audits, thermal distribution uniformity, and total cost of ownership (TCO).
CE marking on industrial storage systems confirms adherence to essential safety, health, and environmental protection standards across the European Economic Area. Unlike general warehouse storage, medical-grade racking requires complex load-deformation metrics under static, dynamic, and seismic operational conditions.
Biologics, vaccines, and temperature-sensitive drugs require strict temperature maintenance within cold rooms (+2°C to +8°C) and deep-freeze environments (-20°C to -30°C). Conventional open-channel racking in deep-freeze environments often experiences brittle fracture risks or disrupts forced-air convective circulation.
In cleanrooms, quarantine staging zones, and packaging suites, dust buildup and microbial harborage are severe compliance threats. Racking systems designed for pharmaceutical factories incorporate explicit hygienic design principles:
A comparative engineering evaluation to help procurement officers and supply chain directors match warehouse operational requirements with the ideal storage architecture.
| Racking Architecture | Storage Density | Pallet Selectivity | Thermal Distribution | Cleanroom Suitability | Primary Pharma Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | Standard (100% Aisles) | 100% Direct Access | Excellent Air Circulation | High (ISO 7 / 8 Ready) | Mixed SKU Finished Goods, High-Velocity Distribution |
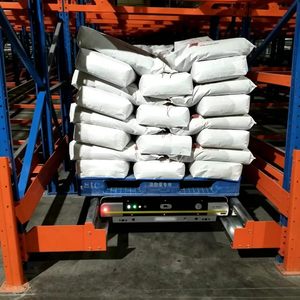
| Automated Radio Shuttle | Ultra-High (Up to 85%) | LIFO / FIFO Automated | Optimized Flow Channels | Medium to High | Cold Storage Vaults, Bulk Vaccine & Biologic Reserve |
| Pallet Flow Racking | High (Gravity Driven) | Strict FIFO Rotation | Good Longitudinal Flow | Standard Warehouse | Date-Sensitive Products, Active Ingredients (APIs) |
| Drive-In / Drive-Through | Very High (Reduced Aisles) | LIFO (Drive-In) / FIFO | Moderate (Density Block) | Moderate | Raw Material Staging, Large Batch Bulk Chemicals |
| Classified Heavy-Duty Mobile Racking | Maximum (80%+ Space Saved) | 100% Selective when Open | Good in Open Position | High | Controlled Substance Vaults, High-Value API Storage |
How industry automation, green manufacturing standards, and smart logistics are redefining the next generation of pharmaceutical storage infrastructure.
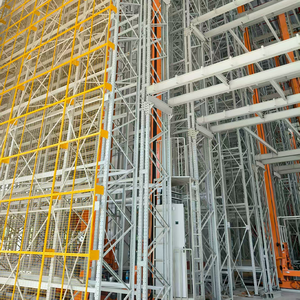
Traditional forklift-operated selective racking is rapidly giving way to AMR-compatible and Automated Storage and Retrieval Systems (AS/RS). Modern pharmaceutical rack engineering integrates micro-tolerance beam levels, laser reflection sensors, and rack-guided shuttle tracks. These systems facilitate human-less, high-velocity picking while minimizing physical contamination risks inside cold rooms and clean staging bays.
Smart racking installations are adopting wireless strain gauges and IoT vibration sensors embedded directly into critical upright frames. Procurement teams are prioritizing racks capable of real-time load displacement logging and immediate forklift collision reporting, interfacing seamlessly with Warehouse Management Systems (WMS) to prevent catastrophic rack failures before they occur.
Global pharmaceutical corporations are accelerating scope 3 decarbonization mandates. Future procurement specs demand low-carbon recycled steel frames produced via electric arc furnaces (EAF) paired with VOC-free, heavy-metal-free powder coatings. Sustainable sourcing standards will be mandatory across all European and North American pharma plant expansions.
With increasing regulatory oversight around track-and-trace serialization (DSCSA and EU FMD compliance), future pharma pallet racking requires modular, lockable wire-mesh enclosures, biometric access gates, and compartmentalized heavy-duty shelving. This ensures segregated storage for Schedule II-V controlled substances and high-value oncology therapeutics.
Addressing key engineering, regulatory certification, export logistics, and installation queries for international pharmaceutical factory projects.
CE compliance for industrial pallet racking involves certifying structural calculations according to EN 15512 standards. We supply a complete technical dossier including Declaration of Performance (DoP), factory production control (FPC) audit reports, raw material certificates (EN 10204 3.1), and stamped structural engineering drawings indicating safe working loads.
Our pharma-grade thermosetting powder coatings utilize high-crosslink epoxy resins that resist degradation from harsh sanitizing chemicals, including peracetic acid, quaternary ammonium compounds, and 70% IPA solutions. Surfaces are non-porous and cured at 200°C to eliminate micro-voids where contaminants could lodge.
Yes. Our shuttle racking channels are precision-extruded from structural steel with exact guide-rail tolerances (±1.0 mm). We integrate proximity sensor cutouts, mechanical end-stops, and sub-zero battery charging stations designed specifically for major third-party wireless radio shuttles operating in cold chain vaults.
Uprights and beams are bundled using heavy-duty plastic strapping, corrugated edge protectors, and VCI (Vapor Corrosion Inhibitor) stretch wrap. Components are packed onto wooden skids certified under ISPM 15 heat treatment standards, optimized for sea container loading with custom piece-level tagging for quick site installation.
Consult with our senior structural engineers to receive customized CAD layout drawings, finite element load analysis, and competitive factory-direct pricing for your pharmaceutical facility.